Engineered for Thermal Regulation, Medical Grade Comfort, and Industrial Durability
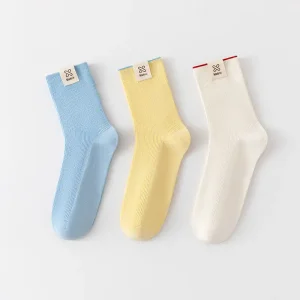
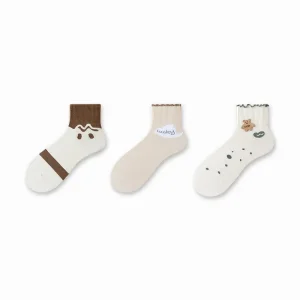
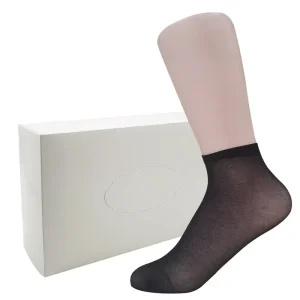
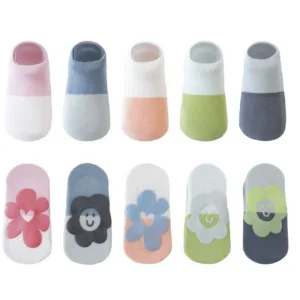
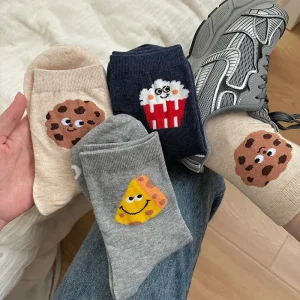
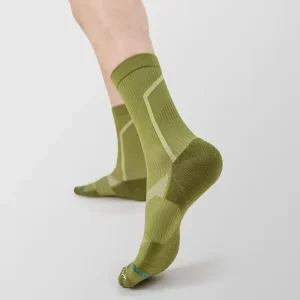
Unlocking Maximum Information Gain and Semantic Authority in Modern Hosiery Manufacturing
The modern global textile landscape has evolved far beyond basic aesthetic comfort. As a leading manufacturer and factory cluster, supplying high-quality Thermal Healthcare Socks demands an intricate balance of biomedical textile engineering and advanced thermodynamic properties. Institutional buyers, clinical distributors, and multinational retail chains increasingly require verified compliance, superior thermal retention, and moisture-wicking efficacy. Our manufacturing paradigm integrates smart yarn selection, computer-aided circular knitting, and rigorous multi-stage quality control to fulfill stringent international specifications.
Global enterprises demand customized supply chain resiliency. By leveraging automated production lines and massive vertical integration, we deliver over 200 million pairs annually to more than 100 countries, ensuring zero stockouts and uncompromised structural integrity for bulk B2B purchasers.
Driven by innovations in phase-change materials (PCMs) and antimicrobial silver-ion infusions, the future of thermal healthcare hosiery lies in active biometric feedback and localized thermoregulation. Our research and development roadmap focuses on seamless graduated compression combined with far-infrared emitting yarns, designed to enhance peripheral microcirculation for diabetic and geriatric care.
Looking toward 2030, sustainable manufacturing is at our core. Utilizing recycled bamboo fibers, organic merino wool, and closed-loop water dyeing systems, our factory meets ISO and OEKO-TEX standards, aligning industrial output with global green energy directives.
The global valuation of specialized healthcare and thermal socks continues its upward trajectory toward the $100 billion threshold. Key growth vectors include aging demographics in North America and Europe, rising participation in outdoor winter athletics, and institutional requirements within healthcare facilities. Operating from our 42,000-square-meter smart facility in Sichuan, we bridge the gap between cost-effective bulk production and elite, medical-grade compliance.
24/7 Performance Armor for Active Lifestages
Zero-Gap Customization: Seamless Journey from Concept to Delivery
Decade-Long Expertise in Hosiery Innovation & Global Export Excellence
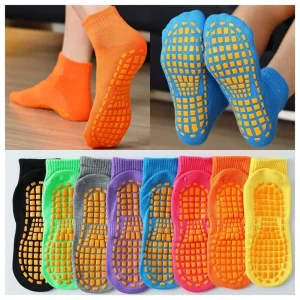
Established in 2013, Sichuan MiFo Technology Co., Ltd. operates a massive 42,000-square-meter factory base equipped with advanced digital looms and testing labs. We specialize in 5 core series: Anti-Slip & Trampoline Socks, Sports & Compression Socks, Disposable Socks, Daily Wear, and Infant Hosiery, exporting to over 100 countries.
Read MoreEstablishment Year
Factory Floor Space (㎡)
Annual Production (Pairs)
Global Export Countries
"Unbroken Promises: 99.4% On-Time Delivery Since 2015"
Full-range socks customization with streamlined global logistics, backed by multinational brand experience.
BSCI/Sedex certified production guarantees socially compliant exports and supply chain integrity.
Co-develop differentiated socks using R&D in antibacterial, thermoregulation, and compression tech.
Mass-scale production ensures on-time delivery for bulk orders, eliminating stockouts securely.
Rigorous quality systems ensure consistent reliability, reducing defects and cutting client costs.
Leverage scale-driven raw material pricing and automation for best-in-class market value.
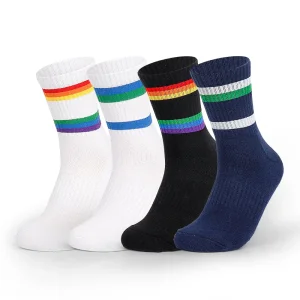
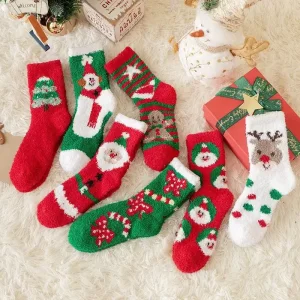
Category Champions: Engineer-Approved, Market-Tested Global B2B Best Sellers
Expert Insights into Global Compliance, Localized Support, and Procurement Logistics
Our production lines are fully certified by BSCI, Sedex, and OEKO-TEX Standard 100. This ensures that all materials used in medical and thermal socks are free from harmful substances and meet rigorous global social accountability standards.
Yes. We offer zero-gap OEM/ODM customization. You can specify exact yarn blends—such as merino wool, bamboo charcoal, or copper-infused fibers—along with targeted graduated compression zones for clinical or athletic requirements.
To maintain high production efficiency and cost-effectiveness, our typical MOQ starts at 1,000 to 3,000 pairs per color/design, though flexible terms can be arranged for enterprise-level trial orders.
We partner with leading global logistics providers (DHL, FedEx, maritime freight forwarders) to offer DDP, FOB, and CIF terms. Our documentation team provides complete origin certificates and compliance paperwork for seamless customs clearance.
Partner with China's premier hosiery manufacturer. Fill out the form below to receive a rapid, accurate quotation.
 MIFO